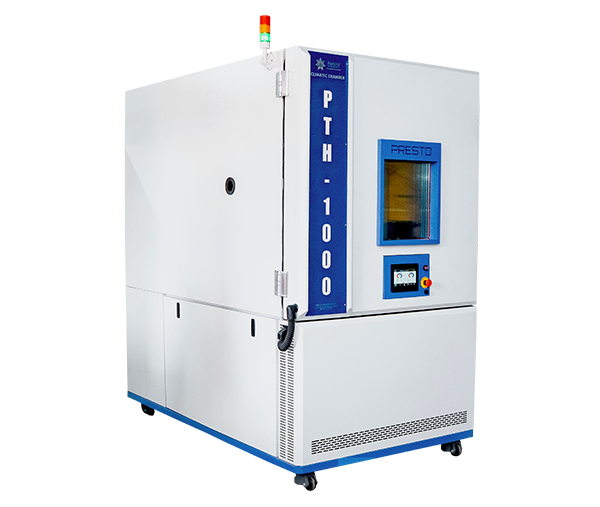
Every modern product needs proper climate testing before launch. A humidity chamber creates accurate climate controls to assess product stability under extreme stress. Choosing the right top humidity test chamber manufacturer for controlled environmental testing ensures long-term equipment accuracy and reliable results. Quality testing prevents expensive product failures and costly recalls down the road. Reliable chambers give engineering teams confidence in every product batch they send to market worldwide.
Top Humidity Test Chamber Manufacturer Solutions for Testing
Selecting proper environmental test equipment protects overall product quality and brand safety. Understanding leading producers helps facilities choose reliable machinery for long term research needs.
Presto Enviro
Presto Enviro stands out as a top humidity test chamber manufacturer for diverse industrial facilities. The company builds reliable units designed for demanding daily quality control workflows across many sectors. Engineers rely on these machines to recreate harsh moisture conditions with complete accuracy.
Each system features easy digital controls and solid steel construction. The internal sensors respond fast to maintain uniform climate conditions throughout the internal volume. Users can easily track real time data for audit compliance and reporting.
This company offers custom build sizes to meet unique laboratory spaces. Their dedicated technical support team helps install equipment and keeps calibration accurate over time. Facilities choose this brand for durable builds and dependable everyday operation.
Modern factories use a Presto Enviro humidity chamber to test sensitive components safely. Reliable moisture control ensures materials do not degrade under unexpected atmospheric changes during global shipment. Solid construction keeps operational costs low for busy testing centers.
Thermotron Industries
Thermotron Industries provides robust equipment built to satisfy strict military and commercial testing protocols. Their advanced humidity test chamber units accommodate large component volumes while maintaining tight climate control parameters. Facilities trust these systems to evaluate heavy electronic assemblies under simulated weather stress.
The intuitive software allows custom profiles for complex multi stage testing routines. Stainless steel interior walls resist rust and chemical damage over years of constant use. High airflow circulation prevents hot spots from forming inside the workspace.
Every unit meets global quality standards to support international compliance needs. The modular design simplifies routine maintenance and system upgrades as testing demands grow. Reliable refrigeration components keep power use efficient during extended operational cycles.
Engineers appreciate the precise relative humidity regulation across broad temperature ranges. Working with a skilled humidity test chamber manufacturer ensures seamless integration with existing lab software setups. Long product lifespans make these systems a smart capital investment.
Weiss Technik
Weiss Technik builds high precision climate equipment designed for demanding research environments. Their state of the art humidity chamber models feature eco friendly refrigerants and energy saving power systems. Quality control teams use these systems to perform accurate stress tests on delicate components.
The digital interface lets operators monitor test parameters remotely with total confidence. Quiet operation makes these units suitable for standard research laboratory floors. Consistent airflow guarantees uniform condition profiles across every shelf position inside the main cabinet.
Advanced steam generators produce rapid humidity changes without overshoot errors. Durable door seals prevent thermal leaks during intense multi day stress routines. Clean design elements make routine sensor maintenance quick and simple for lab technicians.
Researchers depend on every humidity test chamber for reproducible stress data. Precise sensors record small shifts in environmental parameters for deep product analysis. Superior engineering protects test items from unexpected condensation drops during rapid cycles.
Key Factors in Selection
Buying a humidity test chamber requires careful evaluation of core technical specifications. Facilities must measure available floor space and check utility connection limits before purchase. Temperature range capabilities must match expected real world stress scenarios for your target market.
Airflow velocity and interior shelf capacity influence total test volume throughput. Good data logging capabilities streamline compliance verification for strict industry audits. Choosing a reputable humidity test chamber manufacturer ensures quick access to replacement parts when needed.
Conclusion
Controlled environmental testing protects product durability and preserves brand trust across global markets. Deploying a high quality humidity chamber uncovers hidden material flaws long before full mass production begins. Trusted equipment suppliers provide the tools and support required for repeatable test results.
Presto Enviro offers exceptional chamber options alongside Thermotron Industries and Weiss Technik. Investing in dependable climate equipment ensures your testing lab operates at peak performance for years to come.